Weran Solar Weran Solar hWeran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar Weran Solar
Industry News

Home / News / Industry News / Maximizing Energy Yield: How HPBC 2.0 Reshapes BC Solar Module Choices
Industry News

Maximizing Energy Yield: How HPBC 2.0 Reshapes BC Solar Module Choices

How Does HPBC 2.0 Technology Reshape BC Solar Module Selection for Utility and C&I Projects?

Conventional crystalline silicon panels place metal grid lines on the front surface of the cell to collect current. That grid blocks a portion of incoming sunlight, and every busbar or finger printed across the surface represents lost photons that never reach the silicon. Second-generation back-contact technology moves the entire electrode structure to the rear of the cell.

This is not a cosmetic change. Removing front-side metallization eliminates the shading losses that typically account for a measurable share of a module's theoretical output. Combined with an N-type silicon base, which generally offers longer minority carrier lifetime and lower sensitivity to common wafer impurities than P-type wafers, the result is a cell architecture that starts from a higher efficiency ceiling before any downstream engineering even begins.

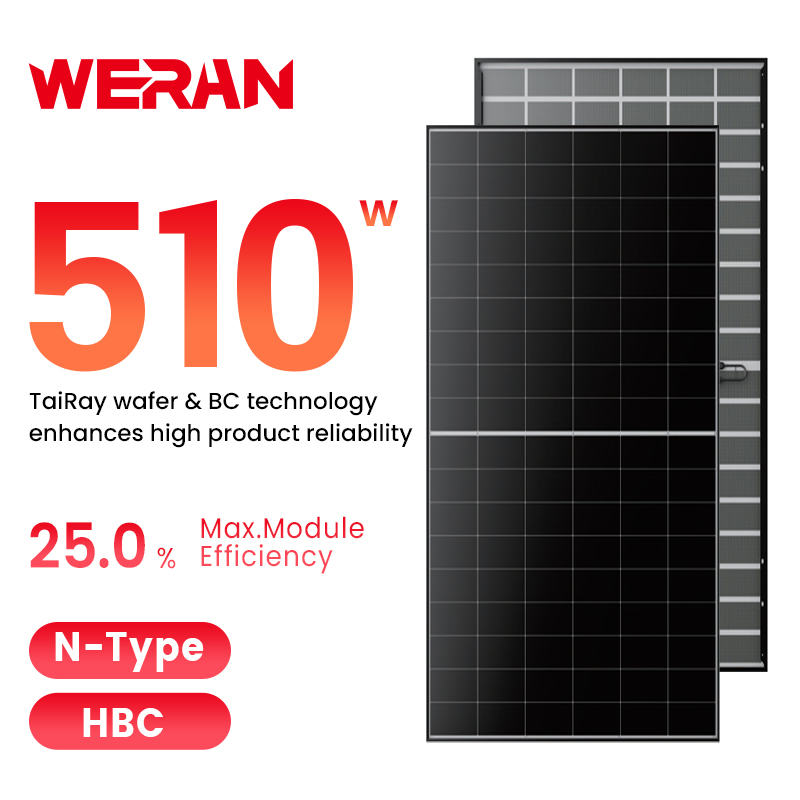
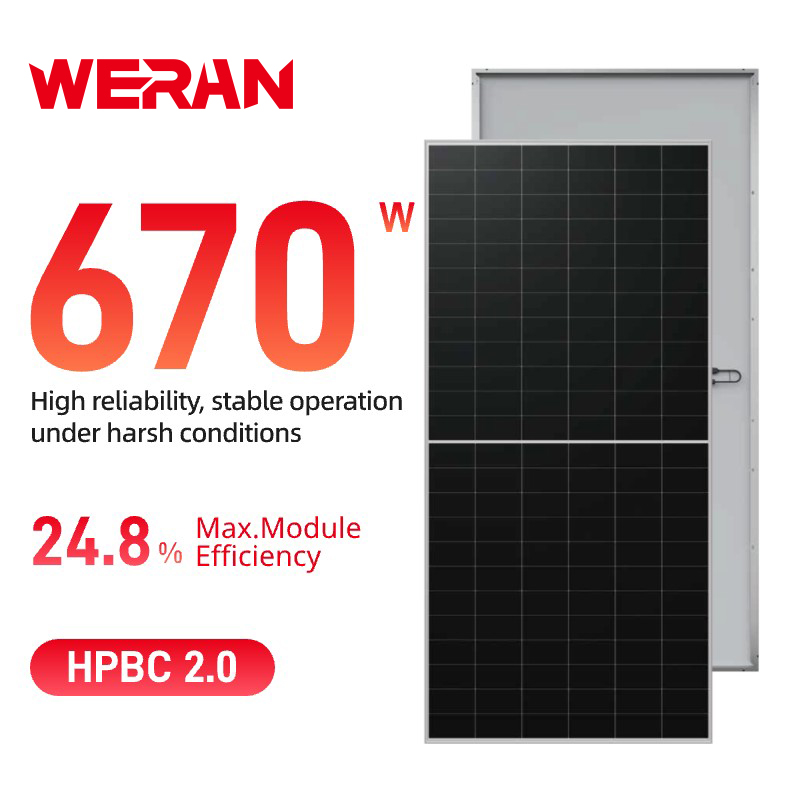
640 to 670 watt back-contact solar module
640-670W Power Class up to 24.6% Max Module Efficiency N-Type Back Contact
01

Why Back Contact Design Reduces Shading and Resistive Losses

Efficiency gains in this generation of back-contact cells come from two compounding effects. First, the absence of front busbars recovers light that would otherwise be reflected or absorbed by metal. Second, because contacts sit on the rear, cell designers can make wider and more numerous narrow-width collecting fingers without creating shade on the front collection surface.

Lower resistance also means the cell runs cooler under equivalent load, which further stabilizes output. When benchmarked against mainstream cell technologies under standard test conditions, the efficiency gap becomes clear.

Module Efficiency by Cell Technology

P-type PERC 21.5% N-type TOPCon 22.0% HPBC 2.0 24.6%

An efficiency improvement of roughly one to two percentage points over TOPCon and PERC alternatives may look small in isolation, but across a twenty-five year service life on a fixed roof area, it compounds into a meaningfully larger total energy harvest, particularly on projects where roof or land area is the binding constraint rather than budget.

02

Thermal Behavior and Power Retention Under Heat Stress

Rooftop and ground-mount modules routinely operate well above the 25 degree Celsius rating condition used on datasheets, with dark composite shingles or low-slope commercial membranes pushing cell temperatures past 55 or even 65 degrees Celsius during peak summer hours.

Every silicon cell loses output as temperature rises, but the rate of loss varies by architecture. Back-contact designs with rear-junction structures tend to be less affected, delivering more effectively than standard back surface field designs, which flattens the output curve as heat increases.

Power Retention vs Cell Temperature

100% 95% 85% 25C 35C 45C 55C 65C
HPBC 2.0Standard BSF

The practical effect shows up most on hot-climate installations and dark roofing or membrane materials, where a flatter thermal curve means the array keeps delivering closer to its rated capacity precisely during the summer afternoon hours when electricity demand and grid pricing are typically highest.

03

Long-Term Degradation and Cumulative Energy Yield

Annual degradation rate determines how much of a module's original output survives after two or three decades of ultraviolet exposure, thermal cycling, and humidity ingress.

A lower first-year degradation figure combined with a slower linear decline thereafter results in a meaningfully larger area under the energy production curve over the life of the system, even when the starting efficiency figure is held constant between two compared platforms.

Cumulative Energy Yield Over 25 Years

Year 5 Year 10 Year 15 Year 20 Year 25
HPBC 2.0Standard PERC

Over a full twenty-five year contract or ownership period, the widening gap between standard degradation curves and HPBC 2.0 decline curves means the incremental energy advantage does not stay fixed at the first-year figure. It grows year over year, which is a critical variable for financial modeling on power purchase agreements and lease structures where revenue is tied directly to metered output.

04

Visual and Structural Advantages for Rooftop Integration

Because the front surface carries no visible busbars or grid lines, back-contact modules present a uniform, dark, continuous appearance that architects and building owners increasingly specify for street-facing rooftops and visible canopies.

This is not purely cosmetic on commercial projects either. A uniform color reduces glare inconsistency across large arrays and simplifies visual inspection during maintenance, since any hotspot or micro-crack tends to stand out more clearly against a clean background.

Relative Attribute Comparison

Efficiency Thermal Degradation Aesthetics Reliability
HPBC 2.0PERC
05

From Wafer to Module: The Manufacturing Flow

Producing a back-contact cell requires tighter process control than a standard front-contact line, since both polarity contacts must be precisely aligned on the same rear surface without shorting. The simplified sequence below outlines the core stages.

Wafer Slicing
->
Doping and Passivation
->
Rear Contact Patterning
->
Lift, Turning and Cleaning
->
Lamination and Framing

Electroluminescence testing after contact patterning is particularly important for back-contact designs, since micro-shorts between adjacent interdigitated fingers are not visible to the naked eye but can measurably affect fill factor. Suppliers with mature back-contact lines typically run full electroluminescence inspection rather than statistical sampling, which reduces the risk of early field failure reaching installed systems.

06

Comparing Total Cost of Ownership: Utility-Scale vs Commercial and Industrial Deployment

Return on investment depends on more than module price per watt. Installation labor, inverter sizing, land or roof area available, and long-term yield all factor into the final calculation. The table below summarizes how module characteristics typically influence project economics across the two most common deployment scenarios.

Factor Utility-Scale Ground Mount Commercial and Industrial Rooftop
Available area Generally abundant, land cost dependent Fixed by roof or canopy footprint
Value of higher efficiency High, reduces land and racking count High, since area is fixed
Value of visual uniformity Low priority in most cases High for street-facing or visible sites
Sensitivity to thermal derating High on open, high-irradiance sites High on dark, low-slope membranes
Impact of slower degradation Improves financing and PPA revenue Improves lease and offset revenue

In both settings, the shared thread is that module economics improve most where the physical constraint is area rather than budget, and where the operating environment includes meaningful heat exposure, which is worth factoring into any project-specific payback calculation.

07

What to Evaluate When Choosing a Supplier

Not every panel labeled as back-contact or N-type delivers the same real-world performance, since cell architecture, passivation quality, and encapsulation materials all vary by production line. Buyers researching bc solar module selection should ask for third-party verified performance data rather than relying on datasheet claims alone, particularly around temperature coefficient and warranty degradation curves.

It is also worth reviewing how a supplier validates its 640-670w solar module line before shipment, including electroluminescence pass rates, hot-spot testing under partial shading, and mechanical load testing for snow and wind conditions relevant to the installation region.

Finally, warranty structure deserves close reading when evaluating the broader hpbc 2.0 technology trend. A meaningful performance warranty should specify guaranteed output at multiple points across the twenty-five year term rather than a single end-of-life figure, since that structure gives a clearer picture of how the degradation curve is expected to behave in practice.

08

Frequently Asked Questions

Q1: What efficiency gains can I expect from standard TOPCon panels compared with back-contact modules?

Second-generation back-contact platforms currently show roughly one to two percentage points of module efficiency advantage over mainstream tunnel oxide passivated contact designs under standard test conditions, though the gap narrows or widens depending on the specific production line being compared.

Q2: Are back-contact panels more expensive than standard modules?

Pricing varies by supplier and volume, but the relevant comparison for a buyer is levelized cost of electricity rather than price per watt alone, since lower degradation and better thermal performance can offset a higher unit price over the system life.

Q3: Is back-contact technology more prone to micro-cracks or reliability issues?

Not inherently. The rear-junction layout requires tighter process control during manufacturing, which is why full electroluminescence inspection and mechanical load testing at the factory level matter more for this architecture than for simpler front-contact designs.

Q4: How does this technology perform in high-humidity or coastal environments?

Encapsulation and frame sealing quality matter as much as cell architecture in these conditions, so buyers in coastal or high-humidity regions should request damp heat and salt mist test results alongside standard efficiency and degradation data before finalizing a selection.